What Is a Rewinding Machine? Types, Process and Selection Guide
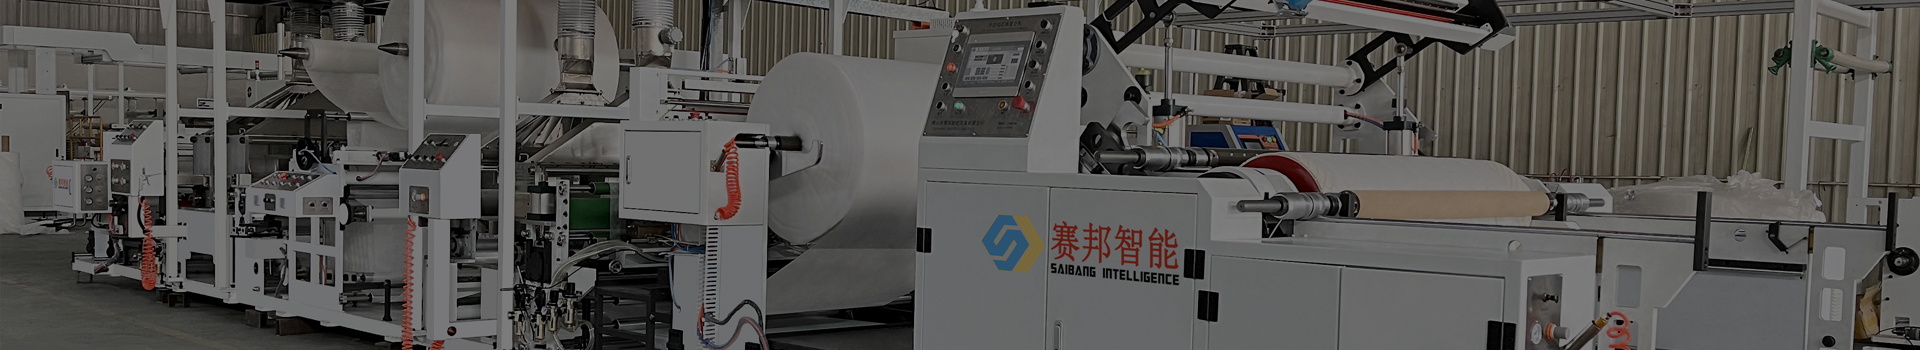
A Rewinding Machine transfers continuous material from a parent roll to one or more finished rolls while controlling tension, alignment, speed, and roll formation. Its configuration should match the material and output requirements.
Why Is Rewinding Necessary?
Large parent rolls are efficient for upstream manufacturing, but downstream users often need smaller, narrower, or differently configured rolls.
Rewinding bridges that gap.
A production line may manufacture material in a wide master roll, while the next process requires:
Narrower widths
Smaller diameters
Different core sizes
Different winding directions
Specific roll lengths
Controlled roll density
The rewinding machine converts the material into the format required by the next production stage.
What Are the Main Rewinding Machine Configurations?
The equipment can be grouped according to its production function.
Basic Rewinder
Used primarily to transfer material from a parent roll to finished rolls.
Slitter Rewinder
Combines width conversion with rewinding.
Multi-Station Rewinder
Uses several winding positions to produce multiple finished rolls.
Automatic Rewinder
Adds automated control functions such as roll change, parameter adjustment, or production monitoring.
Spooling Equipment
Designed around multiple controlled winding positions for reel or spool production.
The appropriate configuration depends on the production target rather than the machine name alone.
What Is the Typical Rewinding Workflow?
A normal workflow looks like this:
1. Parent Roll Loading
The master roll is loaded and aligned on the unwinding section.
2. Web Threading
The material follows the designed roller path.
3. Tension Setup
Initial tension is selected according to the material.
4. Web Guiding
The system maintains lateral alignment.
5. Slitting or Width Conversion
If required, the material is divided into the target widths.
6. Winding
Each web is wound onto its corresponding core.
7. Roll Inspection
The finished roll is checked for diameter, edge condition, density, and visible defects.
8. Unloading
Finished rolls are removed for packaging or downstream processing.
Each step affects the next. A mistake during parent-roll loading can eventually appear as a finished-roll alignment problem.
What Determines Rewinding Machine Size?
Machine size should be based on the largest production requirement rather than the average order.
Key dimensions include:
| Parameter | Why It Matters |
|---|---|
| Maximum Unwind Diameter | Determines parent-roll capacity |
| Working Width | Defines material width capability |
| Maximum Rewind Diameter | Determines finished-roll size |
| Core Diameter | Determines winding compatibility |
| Number of Stations | Determines simultaneous roll production |
| Machine Speed | Affects potential output |
| Floor Space | Determines installation feasibility |
The largest parent roll and finished roll should be confirmed before equipment selection.
How Does Tension Affect the Finished Roll?
Tension is one of the most important process variables.
A tension level that works for one material may be unsuitable for another.
If tension is excessive, the material may stretch or become over-compressed.
If tension is too low, the finished roll may become loose or develop poor edge stability.
More advanced systems can divide tension control into different zones so that the web is managed differently during unwinding, processing, and winding.
Why Does Core Selection Matter?
The core is the foundation of the finished roll.
Its:
Inner diameter
Outer diameter
Length
Material
Strength
can influence winding stability.
The core must be compatible with the winding shaft or spindle.
A mismatch may create poor clamping, eccentric rotation, or unstable roll formation.
For custom equipment projects, core dimensions should be provided before the final winding shaft configuration is determined.
What Is Roll Hardness?
Roll hardness describes how tightly the material is wound.
A roll that is too soft may shift during transportation or downstream feeding.
A roll that is too hard may compress the material or create problems during unwinding.
The ideal hardness depends on the material and its next application.
This is why roll hardness should be treated as a process target rather than simply “the tighter, the better.”
How Should a Rewinding Machine Be Selected?
A useful selection sequence is:
Material first.
Then define:
Width → Thickness → Parent Roll → Core → Finished Roll → Speed → Output → Automation
This order prevents a common purchasing mistake: selecting a machine by speed before confirming whether it can actually handle the material.
What Mistakes Should Buyers Avoid?
Selecting by Maximum Speed Alone
Maximum mechanical speed does not guarantee the same speed in actual production.
Ignoring Finished Roll Requirements
The machine may handle the parent roll correctly but still be unable to create the required finished roll.
Using Generic Tension Settings
Different materials respond differently to tension.
Forgetting Factory Space
Large unwind and rewind diameters can significantly increase machine footprint.
Underestimating Changeover
A machine designed for one product may not be efficient when the factory has frequent width or material changes.
What Should a Factory Provide to the Machine Manufacturer?
A technical inquiry becomes much more useful when it includes actual production information.
The following data should be prepared:
Material sample or specification
Material width
Material thickness
Parent-roll diameter
Parent-roll weight
Core size
Finished-roll width
Finished-roll diameter
Required roll quantity
Target output
Existing upstream equipment
Existing downstream equipment
Material samples are particularly valuable when the substrate is soft, stretchable, layered, or difficult to characterize only by thickness.
How Does a Manufacturer Develop a Rewinding Solution?
The machine should be developed around the customer's actual production process.
Our engineering approach starts by understanding the material and the finished-roll requirement before determining the winding configuration.
The relationship between tension, web guiding, shaft design, winding pressure, roll diameter, and machine speed is then evaluated as one system.
This matters because a rewinder is not an isolated machine. It is part of a continuous production line.
If the upstream machine produces material at one width and the downstream equipment requires another, the rewinder needs to bridge those specifications efficiently.
When Is a Customized Rewinder Necessary?
Customization becomes more useful when standard machines cannot simultaneously satisfy several requirements.
Typical examples include:
Unusually wide parent rolls
Multiple finished-roll widths
Special core dimensions
Delicate materials
Unusual roll diameters
High changeover frequency
Integration with existing lines
Special automation requirements
Customization should solve a defined production problem rather than simply add features.
What Makes a Rewinding Machine Suitable for Long-Term Production?
Long-term performance depends on more than mechanical strength.
A practical industrial rewinder should provide:
Stable web handling
Repeatable tension control
Reliable winding
Accessible maintenance
Consistent components
Clear operator controls
Adaptable production settings
The machine should also be serviceable. Easy access to important components can reduce downtime during routine maintenance.
What Is the Most Important Selection Principle?
The best rewinding machine is not necessarily the fastest or most automated model.
It is the machine whose material compatibility, roll capacity, tension system, winding structure, output, and automation level fit the factory's actual production requirements.
That is the difference between purchasing equipment and engineering a production solution.
Previous: