How Does It Works A Rewinder Machine?
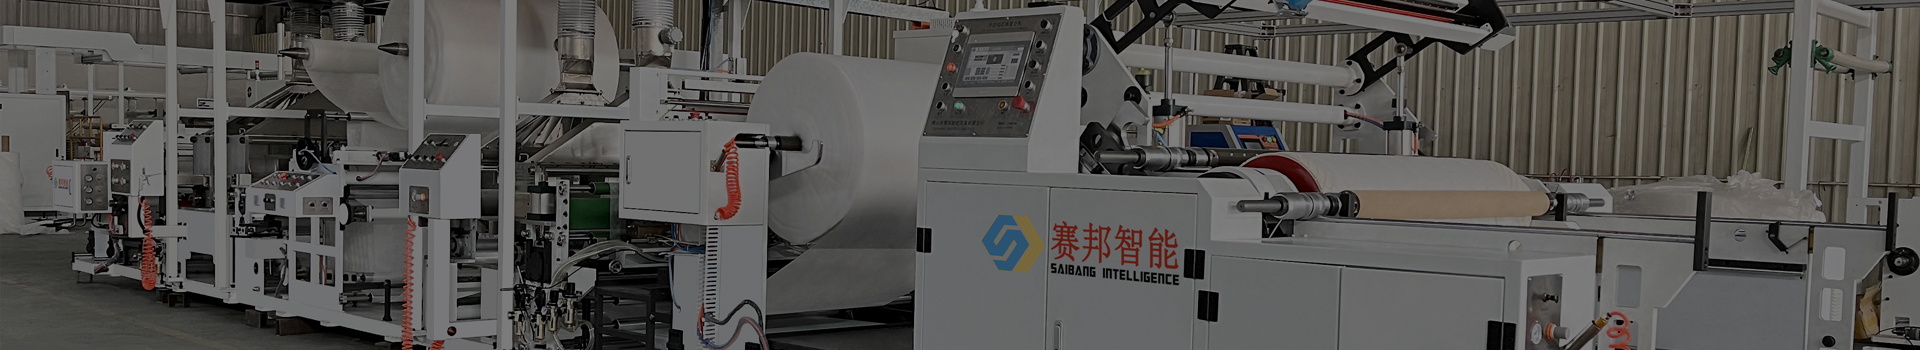
A rewinder machine unwinds material from a parent roll, controls web tension and alignment, and winds the material onto a new core to create a finished roll with controlled width, diameter, and density.
What Is the Basic Rewinding Process?
The basic process follows a continuous web path:
Unwind → Guide → Control Tension → Process or Slit → Align → Rewind
The parent roll is mounted on the unwinding section. The web then passes through rollers and control zones before reaching the winding station.
During this process, the machine continuously manages material movement.
The important point is that rewinding is not simply transferring material from one roll to another. The machine must control how the web behaves while the roll diameter changes.
What Happens at the Unwinding Section?
The unwinding section supports the parent roll and releases material at a controlled rate.
The parent roll must be correctly positioned and secured before production begins.
Important factors include:
Parent-roll diameter
Roll weight
Web width
Core dimensions
Unwinding tension
Roll alignment
If the parent roll is not centered correctly, the web may enter the machine with lateral movement.
That error can then appear later as poor edge alignment or uneven finished rolls.
How Does Tension Control Work?
Tension determines how strongly the material is pulled through the machine.
Too much tension can stretch thin films, deform soft nonwoven materials, or affect laminated structures.
Too little tension can create wrinkles, loose winding, or unstable roll edges.
A rewinder therefore needs a controlled tension profile rather than one fixed value throughout the entire process.
As the roll diameter changes, the required winding conditions also change.
Why Is Web Guiding Important?
Web guiding keeps the material aligned as it travels through the machine.
Even a small lateral movement can become obvious on the finished roll.
Typical web-guiding systems use sensors or edge-detection devices to monitor the web position and make corrections.
The purpose is not to force the material into position aggressively.
The better approach is to make small corrections before the material develops a significant tracking error.
What Happens During Rewinding?
At the winding station, the web is transferred onto a new core.
The machine controls:
Winding speed
Core rotation
Tension
Roll pressure
Edge position
Finished diameter
The result should be a stable roll with consistent density from the core outward.
If the winding force is poorly controlled, defects can develop even when the incoming material was manufactured correctly.
Why Does Roll Diameter Matter?
As a roll grows, its circumference increases.
If rotational speed remained constant, the linear speed of the material would increase continuously.
Therefore, the drive system needs to coordinate rotational speed with roll diameter.
The machine may also adjust tension and winding pressure as the roll becomes larger.
This relationship is fundamental to stable rewinding.
What Are Common Rewinding Defects?
Several defects appear repeatedly in roll-processing operations.
| Defect | Typical Cause |
|---|---|
| Wrinkles | Uneven tension or poor web alignment |
| Telescoping | Lateral movement or insufficient control |
| Loose Roll | Low winding tension or poor pressure |
| Hard Roll | Excessive tension or winding pressure |
| Uneven Edge | Web tracking problem |
| Core Shift | Incorrect core positioning |
| Roll Deformation | Excessive pressure or unsuitable winding conditions |
The same defect can have several possible causes.
For example, wrinkles should not automatically be blamed on low tension. Roller alignment, web tracking, material characteristics, and winding pressure may also contribute.
How Does a Rewinder Handle Different Materials?
The machine configuration must change according to the material.
A thin film may need gentle tension control.
A paper web may require different tension and edge-handling conditions.
A soft nonwoven material can be sensitive to compression.
A laminated web may require careful control to avoid stretching one layer relative to another.
This is why material trials are valuable before final machine parameters are established.
What Is the Difference Between Rewinding and Slitting?
Rewinding changes the roll format.
Slitting changes the web width.
A slitter rewinder combines both functions.
For example, a 2000 mm-wide parent roll may be divided into several narrower webs and then wound into separate finished rolls.
The cutting system determines width.
The rewinding system determines how those cut webs are formed into stable rolls.
Both must be synchronized.
Why Does Machine Speed Not Tell the Whole Story?
A machine may have a high maximum mechanical speed but still operate below that value in real production.
Actual production speed depends on:
Material type
Thickness
Roll width
Tension stability
Slitting method
Finished roll diameter
Operator skill
Product quality requirements
A slower machine that consistently produces usable rolls may provide better production economics than a faster machine that creates high scrap rates.
For equipment selection, stable output speed is more useful than maximum speed alone.
What Does the Operator Usually Adjust?
Depending on the machine configuration, operators may control:
Line speed
Tension
Roll diameter
Winding pressure
Web-guiding position
Core settings
Slitting position
Acceleration and deceleration
Modern controls can make these adjustments more repeatable.
For factories with multiple products, saving validated parameter groups can reduce setup time between orders.
What Should Be Checked Before Starting a Rewinding Job?
A practical pre-start inspection includes:
Confirm the correct parent roll.
Check core size and condition.
Verify web path.
Confirm roller cleanliness.
Check tension settings.
Confirm web-guiding operation.
Inspect winding shafts or spindles.
Start at controlled speed.
Inspect the first finished roll.
Adjust parameters before full production.
The first finished roll is an important quality checkpoint.
It provides evidence of whether the selected tension, alignment, pressure, and winding settings are actually suitable.
How Does Engineering Experience Improve Rewinding Performance?
From a manufacturer's engineering perspective, troubleshooting should start with the entire web path rather than changing one parameter randomly.
If a roll is telescoping, the investigation may include web alignment, tension variation, core positioning, winding pressure, and material behavior.
If the roll is too hard, the solution may involve reducing pressure or tension rather than simply slowing the machine.
This process-based approach helps factories identify the real cause instead of repeatedly treating the visible symptom.
What Is the Core Principle of Rewinding?
A good rewinder keeps three things synchronized:
Material movement
Web tension
Roll formation
When these three conditions remain stable, the finished roll is more likely to have straight edges, consistent density, and predictable downstream performance.
Previous: