What is a Industrial Laminating Machine Production Line and How Does it Work?
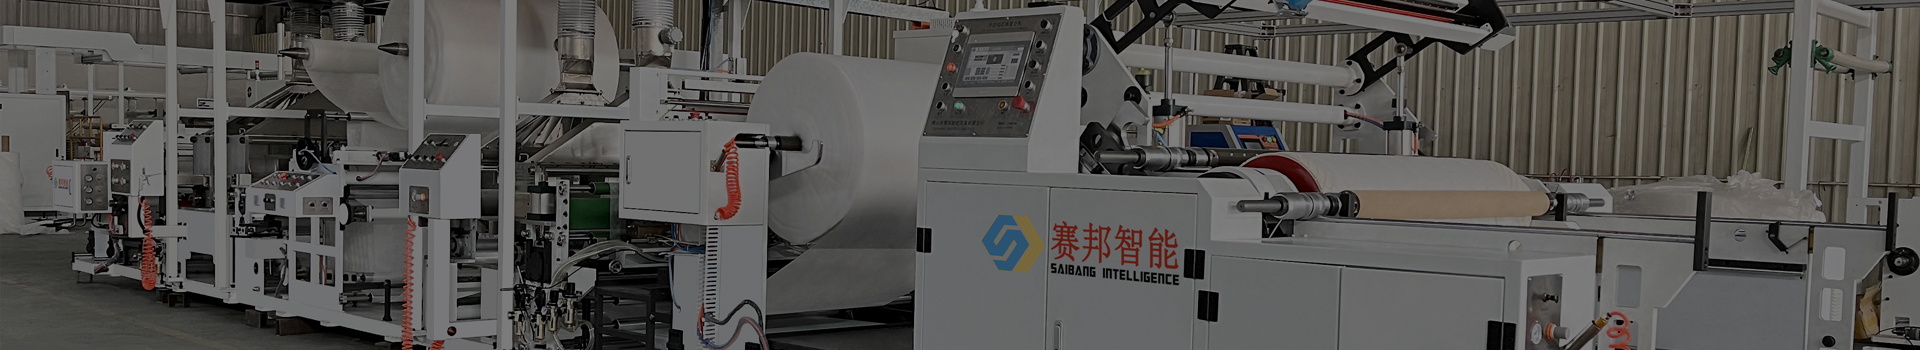
An industrial Laminating Machine production line unwinds, aligns, coats, bonds, presses, cures, inspects, and rewinds multiple material layers into a finished roll.
What Is the Basic Production Sequence?
A typical industrial laminating line follows this sequence:
Load parent rolls
Unwind the substrates
Guide and align the webs
Apply adhesive or activate bonding
Bring the material layers together
Apply controlled pressure
Cool, dry, or cure the laminate
Inspect the finished material
Rewind the finished roll
Every section influences the next one. Poor roll loading may create web movement. Unstable adhesive delivery may cause weak bonding. Incorrect rewinding tension may damage a laminate that was produced correctly earlier in the process.
This is why production-line performance should be measured as a complete process.
What Are the Main Sections of the Line?
Unwinding Units
Unwinding units hold and release parent rolls. Depending on the line design, they may use pneumatic shafts, hydraulic loading, automatic tension control, or automatic splicing.
Web-Guiding Systems
Web guides correct lateral movement and help align the substrates before bonding.
Adhesive Application Units
The coating system applies adhesive at a controlled rate. The application method depends on viscosity, coating weight, production speed, and surface condition.
Laminating Rollers
Laminating rollers bring the layers into contact under controlled pressure. Roller alignment, hardness, temperature, and surface condition influence the final result.
Heating or Curing Sections
Some adhesives require heating, drying, cooling, or moisture-assisted curing. The correct system depends on adhesive chemistry and material structure.
Rewinding Units
The rewinding section forms the finished roll. Tension and roll hardness must be controlled to avoid wrinkles, loose edges, and telescoping.
How Does Tension Control Affect Lamination?
Tension control keeps each web stable while materials pass through the line.
Uneven tension may cause:
Wrinkles
Stretching
Edge displacement
Loose rolls
Excessively hard rolls
Telescoping
Poor slitting results
Different materials require different tension settings. A rigid film, soft nonwoven, paper web, and elastic substrate should not be treated in exactly the same way.
Modern systems may use sensors and drive feedback to adjust tension automatically. Proven settings can also be stored and reproduced for repeat orders.
How Is Adhesive Applied?
Adhesive application depends on the formulation, substrate, coating weight, and target speed.
Common methods include:
Roll coating
Slot-die coating
Gravure coating
Hot-melt application
PUR application
Water-based adhesive application
The application system must control adhesive flow, temperature, viscosity, and distribution.
Excess adhesive increases cost and may affect curing. Insufficient adhesive may lead to delamination, weak edges, or incomplete bonding.
Why Is Pressure Control Important?
Pressure ensures contact between the adhesive-coated substrate and the second material.
Pressure that is too low may result in:
Bubbles
Weak bonding
Incomplete contact
Uneven surface appearance
Pressure that is too high may cause:
Material deformation
Adhesive squeeze-out
Surface marks
Excessive roll hardness
The correct pressure depends on the material thickness, substrate softness, surface structure, adhesive type, and production speed.
What Products Can the Line Produce?
Industrial laminating production lines may be used for:
Flexible packaging
Nonwoven materials
Medical materials
Hygiene products
Protective films
Composite textiles
Industrial fabrics
Paper-film structures
Foil-based laminates
The machine configuration changes according to the application. A hygiene-material line may prioritize cleanliness, soft-web handling, and stable high-speed production. A packaging line may focus on barrier performance, surface appearance, and accurate coating.
The product center covers laminating, slitting, embossing, casting, rewinding, diaper-making, and sanitary-pad-making equipment.
What Quality Tests Should Be Completed?
Machine testing should include:
Roller alignment
Temperature stability
Drive synchronization
Tension response
Adhesive delivery
Web-guiding operation
Rewinding performance
Emergency-stop function
Alarm response
Control-panel operation
Finished laminate testing may include:
Bonding strength
Surface appearance
Coating uniformity
Wrinkle level
Edge alignment
Roll hardness
Delamination resistance
Thickness consistency
Sample trials using the buyer’s actual materials can reveal process limitations before mass production.
How Does Factory Engineering Experience Help?
Industrial laminating projects require knowledge of materials, adhesives, web handling, downstream converting, electrical control, and installation conditions.
The manufacturer’s official information confirms 15 years of R&D experience, more than 30 technical intellectual property rights, CE certification, global supply, and technical support covering installation and debugging.Factory profile
These capabilities help buyers evaluate both the equipment and the complete production process.
What Should Be Included in a Production-Line Proposal?
A detailed proposal should specify:
Machine model
Working width
Production speed
Compatible materials
Adhesive system
Heating or drying method
Tension-control method
Electrical standard
Installed power
Machine dimensions
Spare parts
Training
Commissioning
Delivery schedule
Warranty terms
The proposal should clearly distinguish standard functions from customized modules.
Get a Quote for an Industrial Laminating Line
A technical inquiry should include:
Finished product description
Material samples
Layer structure
Roll width and diameter
Adhesive information
Required output
Production schedule
Factory voltage
Installation space
Destination country
Submit the information through the contact page for a complete production-line evaluation.